

Essential details
MOQ:Min. Order: 1 set
Shipping:Express delivery, air transport, land transport, sea transport
Product Introduction
Product Introduction:
The Axial Replacement Hydraulic Pump is a high-quality axial piston pump designed as a reliable replacement for various hydraulic systems. This robust hydraulic pump delivers exceptional performance and efficiency in demanding mobile and industrial hydraulic applications requiring precise flow control.
Product Image Description:
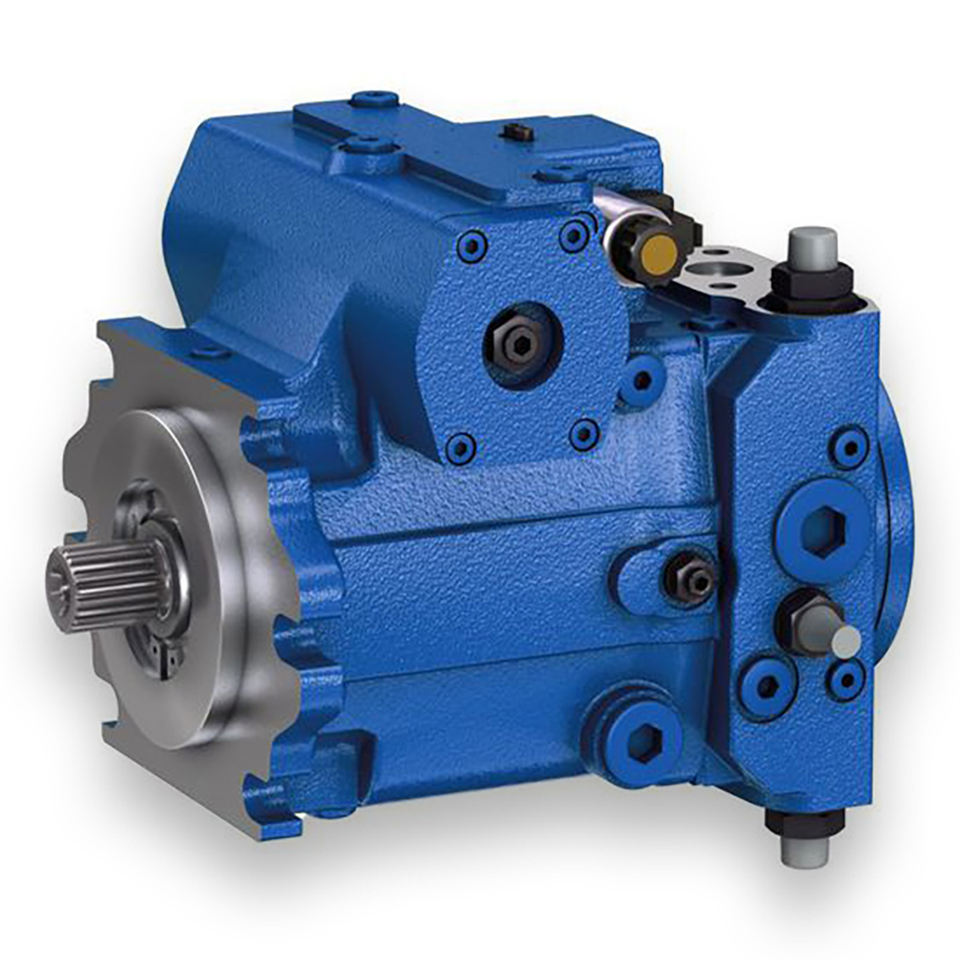
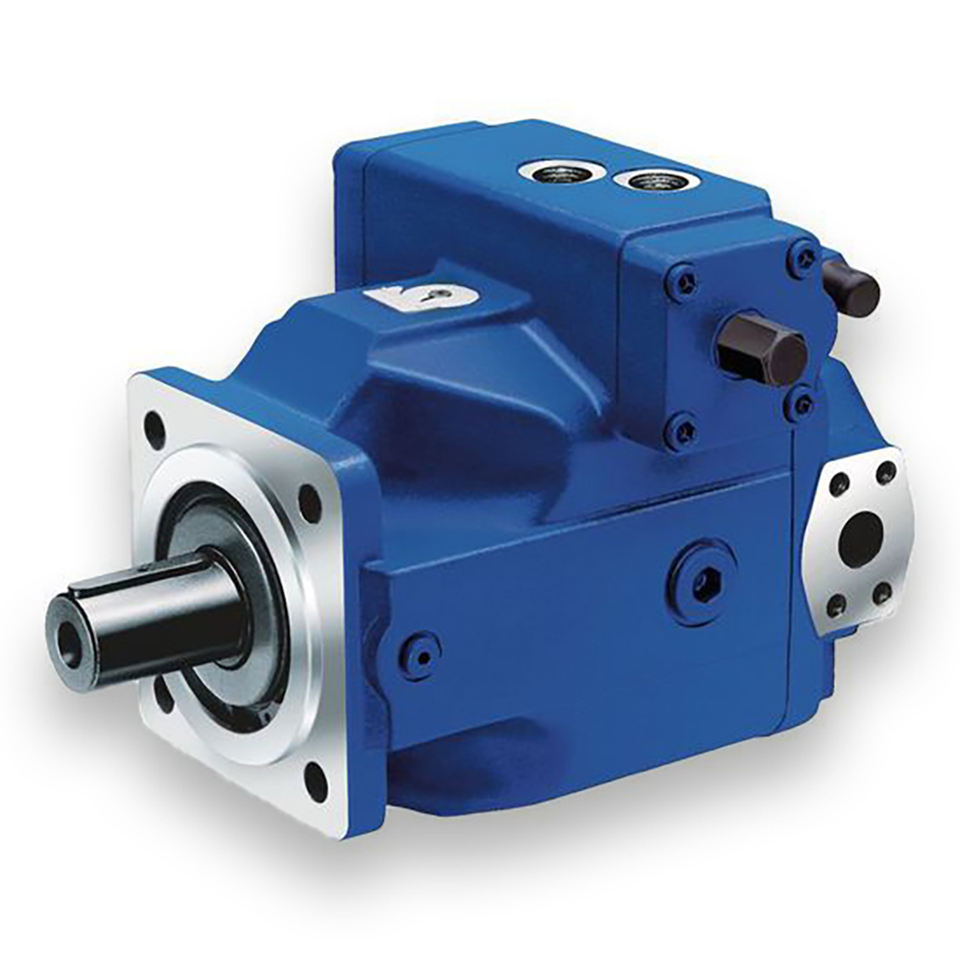
The axial replacement pump features a compact axial piston design with precision-machined components. The unit showcases a durable housing with high-quality internal components including pistons, cylinder block, valve plate, and swashplate mechanism. Multiple mounting configurations and standardized port connections ensure versatile installation capabilities as a direct replacement for original equipment.
Performance Features:
1. Direct Replacement: Designed as a compatible replacement for various original equipment manufacturer (OEM) hydraulic pumps
2. High Pressure Capability: Engineered for continuous operation at rated pressures up to 350 bar with excellent pressure ratings
3. High Efficiency: Optimized axial piston design provides excellent volumetric and overall efficiency across wide operating range
4. Compact Design: Space-saving configuration ideal for mobile and industrial hydraulic applications with limited installation space
5. Low Noise Operation: Precision-balanced rotating assembly and optimized flow paths minimize vibration and noise during operation
6. Long Service Life: Premium materials including hardened pistons and wear-resistant components ensure extended operational lifespan
7. Excellent Control Response: Quick and precise displacement adjustment ensures optimal system performance
8. Wide Operating Range: Suitable for various applications including construction machinery, agricultural equipment, and industrial hydraulics
Additional Information:
- Compatible with mineral and synthetic hydraulic oils (HL, HLP according to DIN 51524)
- Integrated pressure relief valves for system protection and overload prevention
- Easy installation with direct replacement design for minimal downtime
- Meets international quality standards ISO 9001
- Ideal for open circuit hydraulic systems in mobile and stationary equipment
- Suitable for concrete pumps, truck mixers, crane drives, and winch applications
- Self-priming capability with good suction characteristics
- Temperature range: -20°C to +80°C operating conditions
- Bi-directional rotation capability for flexible system integration
- Cost-effective alternative to OEM parts without compromising quality